Food and beverage
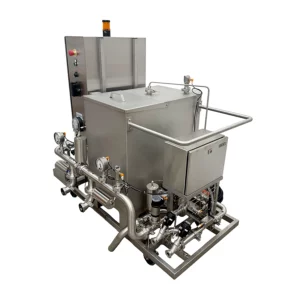
From production to packaging, Pemflow supports the food and beverage industry in managing filtration for processes and utilities.
Our solutions meet the needs of beverage producers, breweries, dairies and sugar manufacturers, with technologies tailored to the requirements of purity, food safety and system performance.
Beverages
For beverage production, Pemflow offers filtration solutions throughout the process, from plant intake to bottling.
Our membranes and filters combine high retention capabilities with resistance to regeneration and sterilisation cycles.
The range meets EN 1935/2004, FDA and ACS requirements, as well as those of the Drinking Water Directive (DWD). Depending on the product, certificates confirming the absence of bisphenols, phthalates or silicone, as well as Halal and Kosher certifications, can also be provided.
Brewing
In brewing, filtration is used at several stages to clarify beer, improve its microbiological stability, extend its shelf life and prepare it for packaging. From pre-filtration to sterile filtration, our solutions are selected with flavour preservation and process optimisation in mind.
The combination of bag filters, lenticular filters and membrane filters covers these different stages with solutions that comply with EN 1935/2004 or FDA requirements.
Dairy products
In dairy, cheese and chocolate production, filtration must meet particularly stringent regulatory and hygiene requirements.
Pemflow offers steam filters, sterile filters and water filters designed for these environments and integrated into various stages of the process.
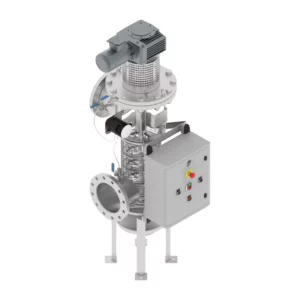
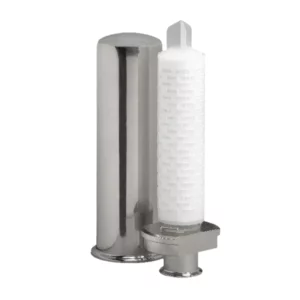
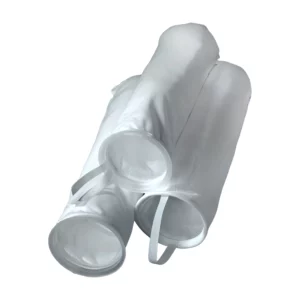
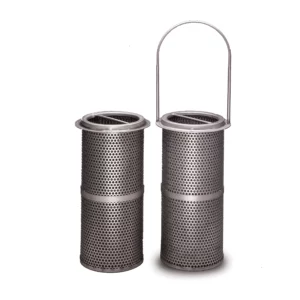
Depending on the application, our solutions use membranes, cartridges, baskets, bags and self-cleaning filters to meet the filtration needs of the most demanding food processing plants.
Sugar production
In sugar production, filtration is required for both syrup and utilities. Our solutions using bag filters, basket filters, cartridge filters or self-cleaning filters are suited to processing highly viscous fluids while achieving the required level of purification.
The range covers various stages of the process with equipment that meets EN 1935/2004 and FDA requirements, helping ensure plant compliance and control fluid quality.